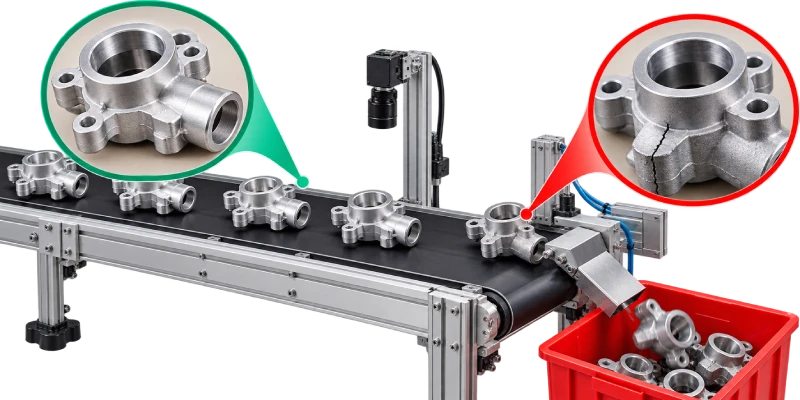
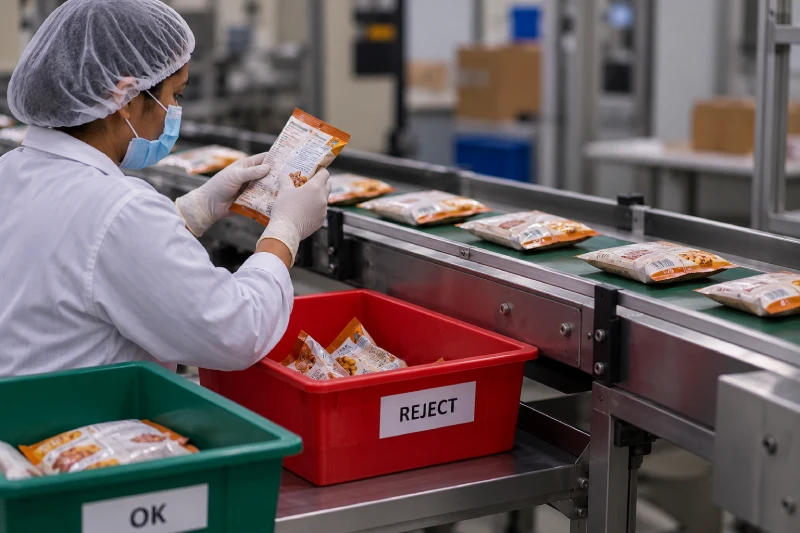
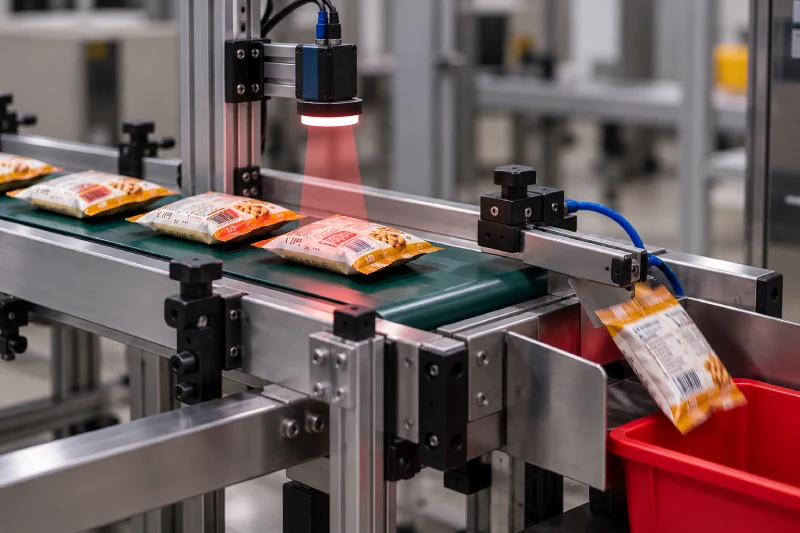
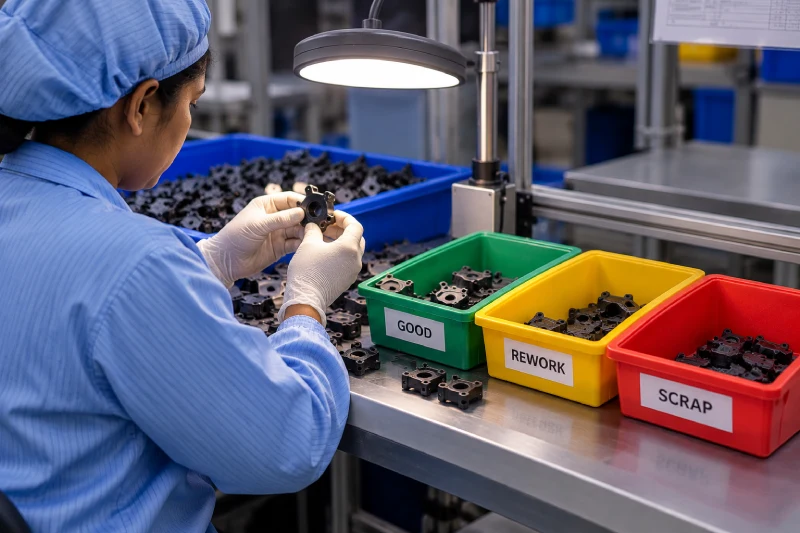
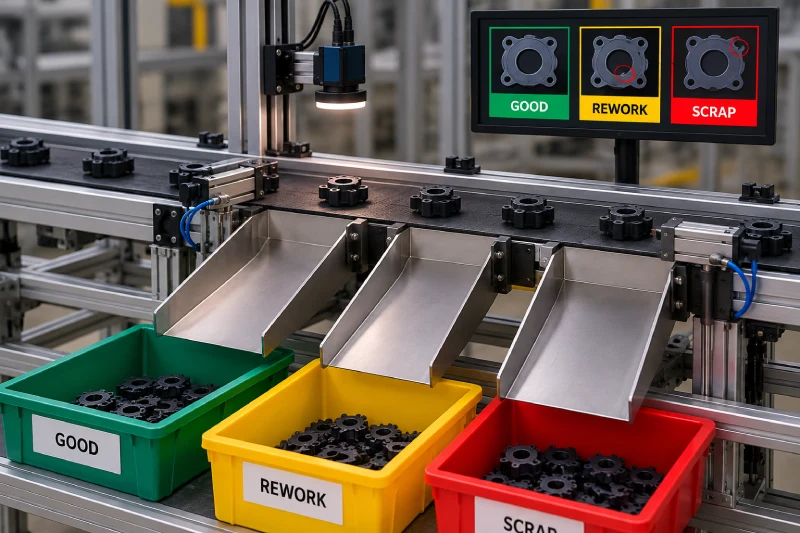
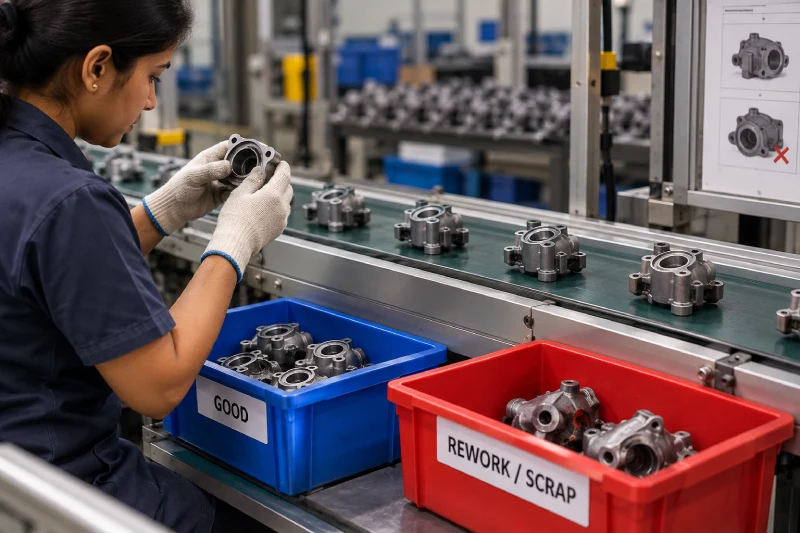
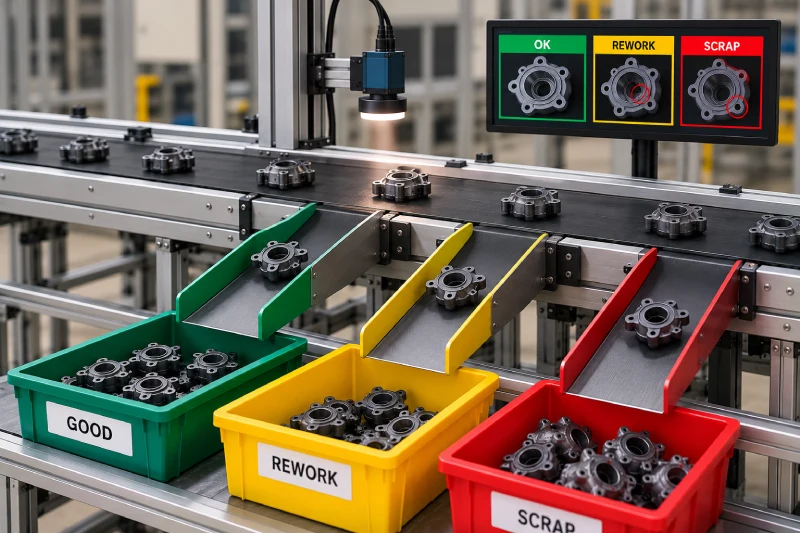
Finding a defect is only half the job. If the rejected part still reaches the next station, the inspection achieved little. The decision has to reach the line in time to act.
We integrate vision with your PLC, reject actuators, and controls so each OK / NG result triggers the right action: air blast, pusher, diverter, alarm, or line stop. Reject tracking, counters, and trends then show where defects start.